Meet Cleanchem Laboratories at Pharmaconex – 01 September, 2026 to 03 September, 2026 • Booth / Stand: Hall 4, Stand #4B22 (Egypt International Exhibition Center, Cairo) – Book an in-person meeting with our scientific leadership team! •••
Details
Downloads
🇬🇧 EN English
🇸🇦 AR العربية
🇨🇳 CN 中文
🇫🇷 FR Français
🇯🇵 JP 日本語
🇵🇹 POR Português
🇷🇺 RU Русский
🇪🇸 ES Español
Compare Cart
Commercial Synthesis Plant 100% ZLD Certified cGMP Compliant Systems

Commercial Chemical Synthesis Plant & Pilot Unit 1

MIDC Industrial Area, Mahad, Maharashtra. Large-scale multi-purpose GMP chemical manufacturing plant featuring 27 Stainless Steel & Glass Lined Reactors (1,000L to 4,000L), 26 Kg/cm² Hydrogenation autoclaves, zero liquid discharge (ZLD) effluent treatment, and dedicated pilot-scale commercial suites.

27 Reactors
16 SSR • 11 GLR (1kL to 4kL)
26 Kg/cm²
2.3 kL Hydrogenation Autoclaves
11 Centrifuges
48”, 36” & 24” Separation Baskets
100% ZLD
ETP Plant & Wet Scrubbers
World-Class Synthesis Hub

Commercial Chemical Synthesis Infrastructure

Our chemical synthesis plant is built with a world-class infrastructure that ensures efficiency, safety, and sustainability in every process. The facility is equipped with advanced reactors, high-pressure vessels, distillation columns, and purification units that enable us to carry out a wide range of complex chemical reactions with precision.
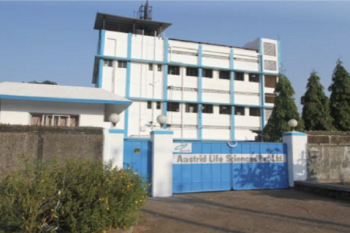
Cleanchem Manufacturing Unit 1 Facility Mahad
Unit 1 Manufacturing Plant
MIDC Mahad • 27 Reactors • 100% ZLD Facility
Automated Process Control
Real-time SCADA and automated DCS monitoring of temperature, pressure, agitation, and dosing for zero deviation.
Real-Time Monitoring
Cross-Contamination Prevention
Segregated modular production suites, isolated packaging cleanrooms, and dedicated solvent transfer loops.
Strict Segregation
Strict Regulatory Adherence
Engineered to comply with global pharmaceutical guidelines, complete batch manufacturing records (BMR), and full traceability.
Global Compliance
Multi-Ton Scalability
Seamless process scale-up from kilogram pilot batches to commercial multi-ton manufacturing campaigns.
kg to Multi-Ton
Synthesis Capacity

Reaction Vessels & Hydrogenation Infrastructure

Equipped with 27 industrial reaction vessels ranging from 1,000L to 4,000L capacity, supported by dedicated high-pressure hydrogenation autoclaves and industrial chilling units.

Stainless Steel Reactors (SSR)
16 Nos
1 kL to 4 kL Capacity
SS316L grade, high-pressure steam/chilled jackets, high-vacuum compatibility.
Glass Lined Reactors (GLR)
11 Nos
1 kL to 4 kL Capacity
Corrosion-resistant glass lining for acidic, halogenating, and aggressive reaction chemistries.
High-Pressure Hydrogenators
2 Units
2.3 kL • Design Pressure 26 Kg/cm²
Advanced catalytic hydrogenation, nitro reduction, and pressurized gas-phase reactions.
Stainless Steel Reactors (SSR)
16 Nos installed with capacities ranging from 1kL to 4kL for basic & neutral campaigns.
16 Nos • 1kL - 4kL
Glass Lined Reactors (GLR)
11 Nos installed for acid chloride, bromination, chlorination, and diazotization steps.
11 Nos • 1kL - 4kL
High-Pressure Catalytic Hydrogenators
2 Hydrogenator autoclaves with 2.3 kL capacity engineered for 26 Kg/cm² pressure rating.
2 Units • 26 Kg/cm²
Dual Industrial Chilling Plants
2 Industrial Chilling Plants operating at 8 TR and 40 TR for rapid exothermic cooling & crystallizations.
2 Nos • 8 TR & 40 TR
Thermopac Heating Unit
Thermic fluid high-efficiency heating system providing stable uniform thermal transfer up to elevated reaction temps.
Thermic Fluid Heat
Dual IBR & Non-IBR Boilers
Continuous high-pressure steam generation capacity from 500 Kg/Hr to 1000 Kg/Hr for distillation & drying.
500 - 1000 Kg/Hr
250 KVA DG Power Backup
Dedicated heavy-duty diesel generator set guaranteeing 100% continuous power during critical synthesis runs.
250 KVA Continuous
Zero Liquid Discharge ETP
In-house biological, physical, and multiple effect evaporation effluent treatment plant recycling 100% of process water.
100% Water Recycled
Isolation & Processing

Downstream Filtration, Centrifugation & Drying

High-throughput isolation and solid-liquid separation equipment engineered for rapid cake de-liquoring, clean solvent displacement, and dust-free vacuum drying.

Industrial Centrifuges (11 Nos)
Top and bottom discharge centrifuges with basket diameters of 48”, 36”, and 24” for high-yield crystalline separation.
11 Units (24" to 48")
FRP Centrifugal Blowers
2 Corrosion-resistant Fiber-Reinforced Polymer blowers for efficient acid fumes and solvent vapor handling.
2 FRP Blowers
Sparkler & Filter Press
3 Sparkler Filters for polish filtrations and 1 heavy-duty Filter Press for large-scale cake dewatering.
3 Sparklers • 1 Filter Press
Industrial Tray Dryers (5 Nos)
5 Multi-trolley hot air and vacuum tray dryers ensuring uniform drying with zero thermal degradation.
5 Tray Dryers
High-Vacuum Ejectors (2 Nos)
Multi-stage steam and water ejectors generating deep vacuum for delicate liquid distillations.
2 Vacuum Ejectors
Multi-Stage Gas Scrubber System
Caustic and acidic packed-column scrubbers for 100% neutralization of process exhaust vapors.
Wet Scrubbers
Effluent Treatment Plant (ETP)
Advanced Multiple Effect Evaporator (MEE) and RO systems achieving zero liquid discharge.
100% Zero Discharge
Dedicated Storage & Packaging Zones
Climate-controlled raw material warehouses and finish good quarantine areas.
cGMP Packaging
Quality Verification

Plant Analytical & Quality Control Instruments

To support rapid in-process monitoring and final batch release, Unit 1 houses an on-site testing laboratory with chromatographic, spectroscopic, and physical analysis equipment.

HPLC Systems
High-Performance Liquid Chromatography for immediate reaction monitoring, purity checks, and assay determinations.
In-Process Purity
GC Instruments
Gas Chromatography for volatile monitoring, reaction completeness, and residual solvent quantification (ICH Q3C).
Residual Solvents
Karl Fischer Titrator
Automated coulometric and volumetric KF titration for rapid, precision moisture content determinations.
Moisture Analysis
IR Spectrometer
FTIR Fourier Transform Infrared Spectrophotometer for instantaneous functional group and identity confirmation.
Structural Identity
Polarimeter
High-precision digital optical polarimeter evaluating Specific Optical Rotation (SOR) and chiral purity.
Chiral Purity
Melting Point Unit
Digital melting point apparatus for rapid thermodynamic identification and crystalline purity checks.
Melting Range
Auto Titrator
Automated potentiometric titrator for acid-base, non-aqueous, and redox assay quantifications.
Assay Testing
Heating Furnace
High-temperature muffle furnace for Residue on Ignition (ROI) and sulfated ash compendial evaluations.
ROI & Ash Content
Commercial Manufacturing Partnerships

Scale Your Chemical Synthesis at Manufacturing Unit 1

Whether you need a custom synthesis batch, contract manufacturing for advanced intermediates, or high-pressure hydrogenation campaigns, our Mahad team is ready to assist.

Schedule Plant Audit
Pharmaconex

Let's connect at Pharmaconex

Cleanchem Laboratories successfully participates in Pharmaconex 2026 at the Egypt International Exhibition Center, engaging with pharmaceutical professionals from Egypt and across the region.

01 September, 2026 Booth Hall 4, Stand #4B22 Egypt International Exhibition Center, Cairo

Cleanchem Support Desk

Online • Scientific Support

👋 Hello! Welcome to Cleanchem Laboratories.

How can our senior analytical & synthesis team assist your project today?

Select an option: